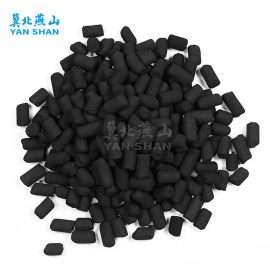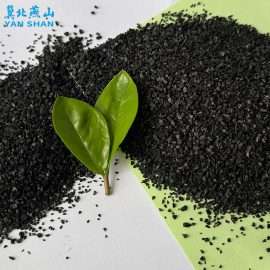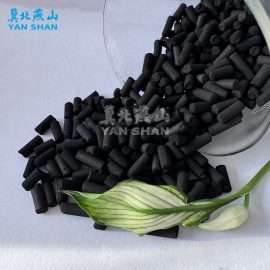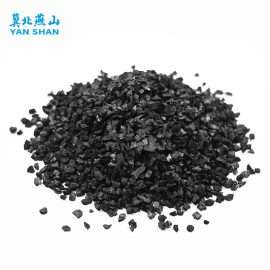


Advantages:
Our coal-based powdered carbon delivers exceptional versatility with rapid kinetics across diverse applications. The optimized particle size distribution creates superior suspension characteristics and maximizes contact efficiency in liquid phase treatments. With its mineral-rich structure, it provides excellent heavy metal binding capacity often missing in biogenic carbons. Process engineers appreciate its consistent iodine number batch-to-batch, ensuring predictable performance. The high bulk density enables more treatment capacity per storage volume. Users consistently report excellent turbidity reduction without excessive head loss. The thermal activation process creates a hydrophilic surface chemistry ideal for polar contaminant removal while maintaining physical robustness under aggressive mixing conditions.
Parameter:
The following is the parameter information of the coal-base activated carbon powder we mainly produce. We can also customize according to the iodine value and specifications you need.
| Item | unit | Index |
|---|---|---|
| Specification100-325 Mesh | % | ≥90 |
| Methylene Blue Adsorption Rate | mg/g | ≥120 |
| Iodine Adsorption Value | mg/g | ≥800-1000 |
| Total Iron Content | % | ≤0.10 |
| Moisture | % | ≤10 |
| Oxide | % | ≤0.20 |
| pH Value | 8 - 10 |
Application:
Chengde Jibei Yanshan Activated Carbon Co., Ltd. is a modern activated carbon production enterprise integrating R&D, production and sales, with rich production experience and advanced technology, and is committed to providing customers with high-quality activated carbon products and perfect solutions.
In addition to this product, our factory also has many other uses of activated carbon. Click below to browse more of our products.